As global manufacturing accelerates its transition toward “cost reduction, efficiency improvement,” and green, low-carbon operations, innovating the formulas for traditional industrial raw materials has become key to a competitive breakthrough. Industry experts note that some ceramic and glass manufacturers still rely on outdated formulas from five years ago, keeping production costs high. Driven by demand in new energy and high-end manufacturing, premium Soda feldspar—characterized by high alumina, high sodium, and low iron content—is rapidly gaining adoption; companies that have upgraded their formulas early on have achieved a cost advantage of over 10% compared to their peers.
Soda ash has long been an indispensable flux in glass manufacturing. However, due to volatile global energy prices and increasingly strict environmental regulations, the price of soda ash has fluctuated wildly in recent years, while its high energy consumption and carbon emissions place immense compliance pressure on enterprises.
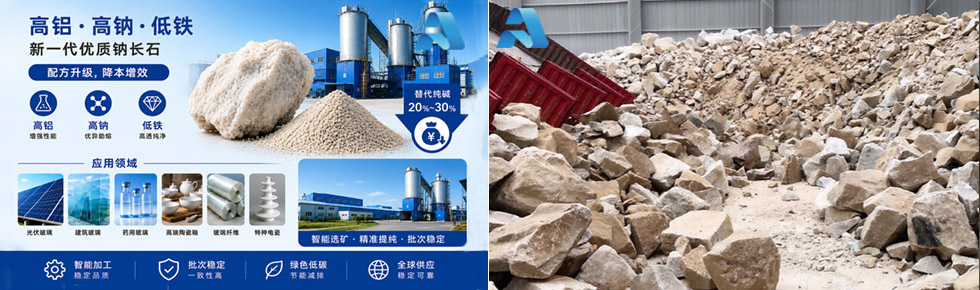
“New-generation premium albite is reshaping traditional formulas thanks to its ‘high alumina, high sodium, and low iron’ properties,” explains a senior industry technical expert. Its high sodium content provides excellent fluxing capabilities; the introduced aluminum and silicon not only simplify the formula but also directly reduce soda ash usage by 20%–30%. The high alumina content significantly enhances the glass’s mechanical strength, chemical stability, and thermal stability while reducing the tendency for devitrification (crystallization). Meanwhile, the low iron content ensures high light transmission and glaze purity. Major players such as Xinyi Solar, Flat Glass Group, and Qibin Group (in the photovoltaic glass sector), as well as architectural glass companies like CSG Holding, have already incorporated this premium albite into their standard formulas, reaping significant cost advantages.
Traditional albite often suffers from issues like fluctuating iron content and low fluxing efficiency. To address this, we are proud to launch a premium albite product—featuring high alumina, high sodium, and low iron content—specifically developed for high-end manufacturing to solve your formulation challenges right at the source! Three core advantages precisely empowering high-end production:
1. High Sodium (Na₂O): Acting as a natural “super flux,” the high sodium content significantly lowers the melting temperature of glass and ceramic glazes. This drastically reduces soda ash usage and directly cuts fuel and raw material costs, resulting in more energy-efficient and productive manufacturing.
2. High Aluminum (Al₂O₃): Strengthens the glass network structure, effectively enhancing the mechanical strength, chemical stability, and crystallization resistance of the finished products. In ceramic applications, it optimizes body density, minimizes deformation, and increases the toughness of the final product.
3. Low Iron (Fe₂O₃): Ultra-low iron content guarantees superior light transmission. Whether for photovoltaic glass, pharmaceutical packaging, or high-end ceramic glazes, this low-iron characteristic ensures crystal-clear transparency and pure colors, easily meeting the rigorous standards of high-end markets.
In the ceramics industry, “high-aluminum, high-sodium, low-iron” albite is rapidly becoming a favorite for glaze formulations, thanks to its low melting point and high fluidity. Experimental data shows that the high sodium content lowers the albite’s melting point to approximately 1100°C. In low-temperature rapid-firing processes, increasing the albite proportion in the glaze to 40% allows the firing cycle to be shortened from 8 hours to 7.2 hours, while the product yield rate jumps from 95% to 98%.
For manufacturers of large-format ceramic tiles, this formulation upgrade offers multiple benefits: the low-iron characteristic reduces glaze cracking rates to 0.8%, while fuel consumption for smart kilns (with a daily capacity of 800 tons per line) drops by 12%, resulting in a CO₂ emission reduction of approximately 15 tons. Industry forecasts predict that by 2026. the adoption rate of this type of high-quality albite in ceramic glazes will exceed 70%.
Our products are also suitable for applications such as photovoltaic glass, pharmaceutical glass, high-end ceramic glazes, fiberglass, and specialty electrical porcelain.
Industry experts emphasize that when evaluating “high-aluminum, high-sodium, low-iron” albite, batch consistency is just as critical as core chemical specifications. As the market share of high-end products continues to rise, upgrading formulations is no longer an “elective” for enterprises—it is a “mandatory requirement” that determines survival. Companies must move away from outdated formulas and deepen technical collaboration with high-quality suppliers capable of stable ore delivery to establish a genuine cost-based competitive moat. We eliminate batch-to-batch fluctuations, safeguarding your production line with consistent quality. Superior raw materials create superior products!
📩 Please send us a private message to request samples and detailed specifications, and let’s unlock new formulas for cost reduction and efficiency gains together!
📞Tel:+86 158 3720 7537 (WhatsApp)
📧Email: info@lsakminerals.com
🌐Web: www.lsakminerals.com

Whether you have questions or you would just like to say hello,Contact us!
Call Anytime:
+86 15837207537Send E-mail:
info@lsakminerals.comAddress:
Anyang City , Henan Province, China.